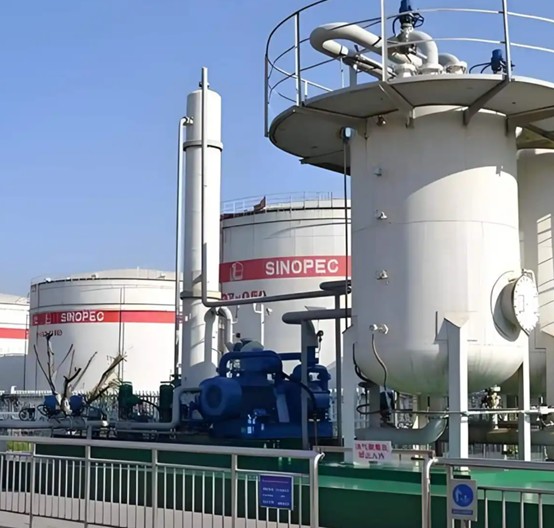
Oil and gas vapor recovery unit searches show that buyers are looking for practical information about capturing hydrocarbon vapors, reducing VOC emissions, and improving product recovery. A VRU can be used at storage tanks, loading points, terminals, and production sites where valuable vapors should be recovered rather than destroyed.
Main VRU page: https://pollutionctrl.com/oil-gas-vapor-recovery-unit/
What a vapor recovery unit does
A vapor recovery unit collects hydrocarbon-rich vapor and separates or compresses it so the recovered vapor can be reused, sold, or returned to a process. The system helps reduce VOC emissions, odor, product loss, and environmental compliance risk.
Common VRU applications
Typical applications include crude oil storage tanks, condensate tanks, gasoline loading, natural gas liquids handling, petrochemical terminals, marine loading, and refinery vapor control. The best system design depends on vapor composition, pressure, flow rate, and recovery target.
Key selection data
Before selecting a VRU, define vapor flow rate, hydrocarbon composition, oxygen content, water content, pressure, temperature, operating schedule, and the destination for recovered vapor. This information affects compressor selection, condensation design, adsorption design, controls, and safety protection.
VRU vs thermal oxidation
A VRU is usually preferred when the vapor has recoverable value or when emissions can be captured efficiently. A thermal oxidizer or RTO may be used when the vapor is not economical to recover, contains mixed VOCs, or requires destruction instead of recovery. Thermal oxidizer reference: https://pollutionctrl.com/thermal-oxidizer/
When RTO backup may be needed
Related equipment pages: Oil & Gas Vapor Recovery Unit | Thermal Oxidizer | RTO for VOC Control | Discuss a VRU Project
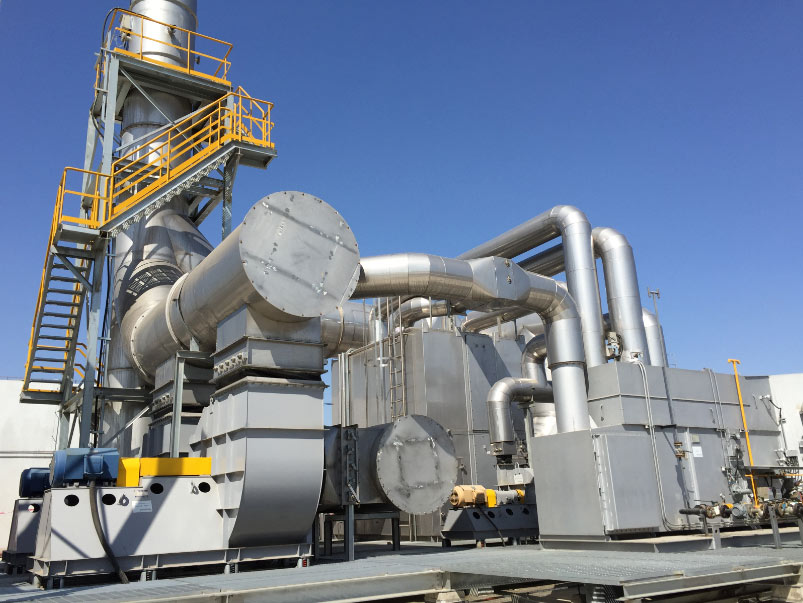
Some oil and gas facilities use destruction technology for non-recoverable vent streams, upset conditions, or mixed VOC exhaust. For VOC destruction equipment, see: https://pollutionctrl.com/regenerative-thermal-oxidizer/
Safety and controls
VRU design must consider flammability, oxygen control, pressure protection, emergency shutdowns, grounding, compressor protection, and local emission requirements. The control system should respond to changing vapor generation rates without creating tank pressure problems.
Maintenance points
Operators should monitor compressor performance, seal condition, condensate handling, pressure control, oxygen alarms, filters, and recovered vapor quality. Unstable pressure or unusual compressor cycling often indicates a process or control issue.
FAQ
What is the difference between vapor recovery and vapor destruction?
Vapor recovery captures hydrocarbon vapor for reuse or sale. Vapor destruction oxidizes VOCs when recovery is not practical.
Where is a VRU used?
VRUs are used at storage tanks, loading racks, terminals, production sites, refineries, and oil and gas processing facilities.
What information is needed to size a VRU?
Flow rate, vapor composition, pressure, temperature, oxygen content, water content, operating hours, and recovery target are the starting points. Request project support here: https://pollutionctrl.com/contact/
Vapor Recovery Technical Resource Center
Need a direct VRU recommendation? PollutionCtrl can compare compression, condensation, adsorption, absorption and vapor combustion from vapor composition, flow, pressure and recovery destination.
- Refinery and tank terminal vapor control systems
- Marine vapor recovery for ship and terminal loading
- VRU troubleshooting: cycling, high pressure and liquid carryover
- Request a vapor recovery equipment review from PollutionCtrl
VRU Selection by Operating Condition
Select a vapor recovery unit from normal and peak vapor flow, tank pressure, gas composition, temperature, liquid carryover, recovery destination and operating hours. Tank farms, terminals, truck loading and gasoline storage can have different vapor patterns and should not be treated as one standard duty.
VRU Equipment Package
A complete oil and gas VRU may include a compressor, inlet separator, liquid handling, controls, valves, instruments, piping and recovery connections. See the VRU manufacturer page, VRU compressor package and VRU design guide before requesting a quotation.
Information for a VRU Quote
Provide tank volume, vapor source, normal and peak flow, pressure range, gas analysis, liquid carryover risk, hazardous-area classification, recovery target and site layout. These details determine the compressor and control arrangement.