Industrial VOC and Odor Control Equipment Selection Guide
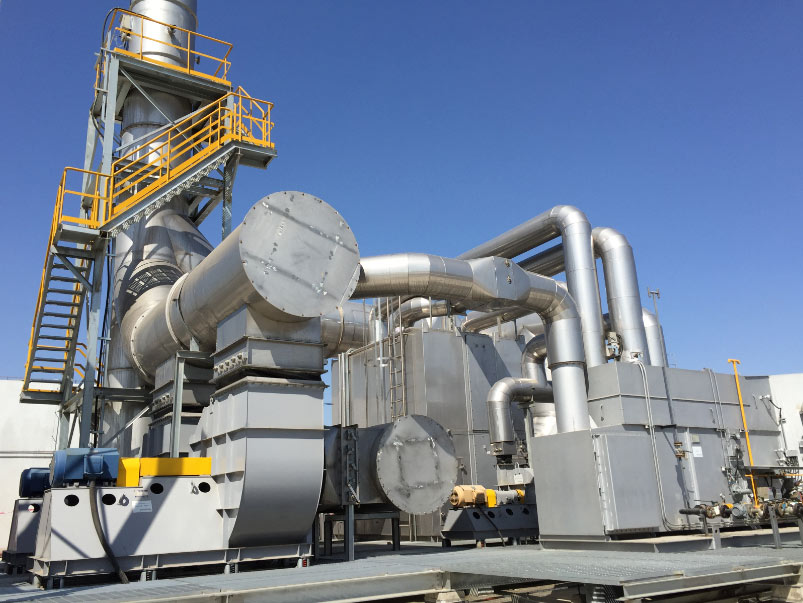
PollutionCtrl supplies industrial air pollution control equipment for VOC treatment, vapor recovery, thermal oxidation, catalytic oxidation, adsorption and odor control. This guide is for plant engineers and procurement leads choosing between RTO, thermal oxidizer, catalytic oxidizer, concentrator plus oxidizer, activated carbon, vapor recovery, scrubbers, biological treatment, plasma and microwave UV oxidation.
Step Zero: VOC Treatment and Odor Control Are Two Different Problems
VOC treatment and odor control are different duties; deciding which applies comes first.
VOC treatment is a mass duty
VOC treatment destroys or recovers a measurable pollutant mass, usually from a defined vent or collected enclosure where flow, temperature, species and concentration are known. Design is driven by concentration, flow, residence time and catalyst compatibility. Oxidation, concentration, adsorption and condensation fit here; start from the VOC treatment system route where a defined concentration and a permit limit apply.
Odor control is a perception duty
Odor control keeps the fence line acceptable. Odor comes from trace sulfur species, amines, fatty acids and aldehydes at concentrations too low to justify high-temperature oxidation, yet detectable off site. Such streams are large, near ambient and moisture-saturated, from wastewater tanks, sludge handling, garbage transfer and rendering. Wet scrubbing, biological treatment, adsorption, plasma and microwave UV oxidation fit here; see industrial odor control systems.
Where the two overlap
A wastewater area can release odorous traces and a real VOC load at once. Where both apply, a staged train – odor and dust removal, then VOC destruction or polishing – beats one technology stretched across both. See how to choose between RTO, catalytic oxidizer and plasma odor control.
The Selection Decision Tree
Work the four steps in order; naming a technology earlier is why projects get re-scoped late.
Step 1 – Concentration and flow rate first
Dilute high-volume streams are the hardest to oxidize economically: heating a big gas volume that carries little pollutant is disproportionate to the mass removed, so concentrate them first with a rotary concentrator with thermal oxidizer or activated carbon adsorption with catalytic combustion. Medium concentration at medium to high flow is the classic regenerative thermal oxidizer case, while concentrated low-flow streams, or those whose product has value, favour a thermal oxidizer or condensation and vapor recovery. Check how close concentration sits to the lower explosive limit; that alone changes the safety architecture.
Step 2 – Halogens, silicon, phosphorus, dust, moisture
Run the full species list first. Halogens and silicon change the answer outright: they poison or mask catalyst, and halogenated streams change material selection and downstream treatment because the oxidation product is acidic. Dust, mist and particulate need pre-filtration whatever follows, because they foul heat-exchange media, blind adsorbent beds and coat catalyst.
Step 3 – Energy, consumables, by-products
Compare fuel or electrical demand, fan power, catalyst and adsorbent replacement, scrubber chemicals and blowdown, and disposal of spent material. Include start-up and shutdown behaviour: batch processes pay for heating cycles that continuous ones do not.
Step 4 – Compliance limits and space
Fix the two constraints equipment cannot negotiate: the outlet limit and the available space. The limit from your permit sets the removal level and must be defined before design. Space decides whether a large multi-bed unit is feasible or a rotary-valve arrangement is needed. Confirm permit and utility capacity early; authorization timelines are often the critical path.
Technology Comparison for VOC and Odor Duty
| Technology | Applicable concentration and flow | Strengths | Limitations | Typical applications |
|---|---|---|---|---|
| Thermal oxidation – RTO or direct-fired | Medium to high concentration and flow | High heat recovery; tolerant of rich streams | Halogens and silicon affect materials and catalyst; fuel needed at low load | Coating, printing, chemical and petrochemical vents |
| Catalytic oxidation | Low to medium, halogen-free | Lower temperature, lower fuel use, compact | Catalyst poisoned by halogens, silicon, phosphorus or metals | Clean solvent vents, ovens, packaging exhaust |
| Concentration plus oxidizer | Dilute, high flow | Shrinks the volume to be oxidized | Adsorbent replacement; dust and moisture control upstream | Large low-concentration paint and coating exhaust |
| Activated carbon adsorption | Low to medium concentration and flow | Low temperature; good polishing stage | Bed saturation; spent-carbon disposal; heat and moisture cut capacity | Polishing after a main stage; intermittent streams |
| Condensation and vapor recovery | High concentration, low flow | Recovers product instead of destroying it | Deep cooling is energy-intensive; performance falls as concentration drops | Tank breathing; truck and terminal loading |
| Biological treatment (biofilter) | Low concentration, high volume | Low operating cost, no fuel | Slow response to load swings; sensitive to temperature and pH | Wastewater and sludge odor; composting air |
| Wet scrubbing | Water-soluble or reactive species | Handles moisture and particulate together | Weak on low-solubility organics; chemicals and wastewater produced | Odor and acid gases from wastewater and chemical areas |
| Low-temperature plasma | Low concentration, high volume, ambient | Compact; fast start-up | By-product formation must be assessed; dust and moisture control | Wastewater, sludge and transfer station odor |
| Microwave UV oxidation | Low concentration, high volume, ambient | Chemical-free oxidation; fast response | Sensitive to particulate and moisture; best with pretreatment | Wastewater, sludge, garbage and rendering odor |
Use the table to eliminate options, not to pick one. Principles for the compact routes are under low-temperature plasma for industrial odor control and microwave UV oxidation for industrial odor control.
Quick Equipment Selection by Problem
| Problem | Recommended equipment options |
|---|---|
| High-volume VOC exhaust | RTO, thermal oxidizer, catalytic oxidizer |
| Low to medium VOC or odor load | Activated carbon, plasma, microwave UV oxidation, combined process |
| Oil vapor from tanks or loading | Vapor recovery unit or vapor control system |
| Wastewater odor | Plasma, microwave UV oxidation, scrubber, activated carbon, biofilter |
| Sludge or garbage odor | Microwave UV oxidation, plasma, scrubber, activated carbon polishing |
| Catalyst-compatible VOCs | Catalytic oxidizer |
Selection Mistakes That Cause Rework
- Choosing on capital price alone. A cheaper unit can consume more fuel, catalyst, adsorbent or chemicals each year; compare operating inputs over the service life.
- Skipping pretreatment. Particulate, mist and moisture degrade heat-exchange media, catalyst beds and adsorbent beds.
- Sizing on average flow. Peak flow, batch surges and start-up set the size and turndown range; a unit sized on the average is undersized when it matters.
- Ignoring by-products and spent material. Acid gases, scrubber blowdown, spent carbon and catalyst, and biological sludge all carry disposal consequences.
Process Data to Collect Before Requesting a Quote
- Gas source and where the stream is captured
- Design and normal flow rate, with peak and minimum cases
- Pollutant list with concentrations, and a full species list where available
- Odor description and any component or sensory target
- Inlet gas temperature and moisture content
- Dust, mist and oil content, with any pretreatment installed
- Presence of halogens, silicon, phosphorus, sulfur or heavy metals
- Required outlet limit or removal level, and the basis it comes from
- Explosion risk assessment and flammable-range considerations
- Operating hours and pattern – continuous, shift, batch or seasonal
- Ambient conditions, elevation, noise and footprint limits, plus space for pretreatment and ducting
- Available utilities: fuel, electrical capacity, air, water, drainage, and tie-in points
Send the list even if some items are approximate; missing data is easier to resolve at proposal stage than after the equipment is sized.
Frequently Asked Questions
What is the best VOC control equipment?
There is no single best option; RTO, thermal oxidizer, catalytic oxidizer, activated carbon, vapor recovery and combined systems are chosen by concentration, flow and gas composition. Eliminate technologies your gas cannot tolerate, then compare the survivors on lifecycle cost.
What is the best equipment for wastewater odor?
Source enclosure with negative-pressure collection, then plasma, microwave UV oxidation, wet scrubbing, activated carbon or biological treatment. Collection is often the more important half, because a treatment unit cannot remove odor that never reaches it.
When should a vapor recovery unit be used?
When hydrocarbon vapor can be captured and recovered from storage tanks, truck or terminal loading, or process vents. It suits concentrated streams, not dilute ones.
Do I need pretreatment before an oxidizer or adsorption system?
Yes, in most installations. Particulate, mist and moisture foul heat-exchange media, poison or mask catalyst and blind adsorbent beds, so pretreatment belongs in the same selection.
Talk to an Engineer
Send your stream data – flow, concentration, pollutant list, temperature, moisture, dust and outlet limit – with the site constraints. Tell us which duty applies, or whether both do, and we will return a preliminary technology route and equipment scope. Contact our engineering team to start the review.