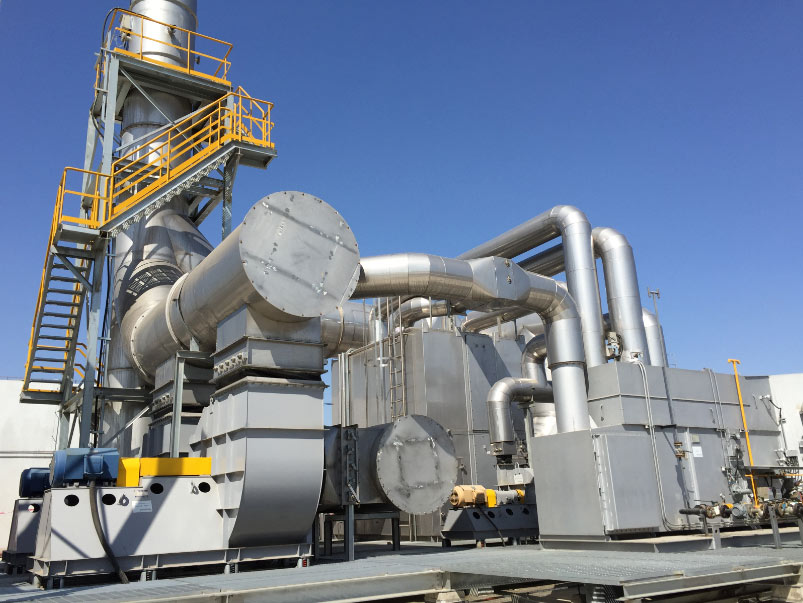
A vapor recovery unit compressor boosts recovered hydrocarbon vapor to a pressure where it can be condensed or absorbed into liquid product. Compressor selection is a critical part of VRU design, matched to vapor flow, composition and discharge pressure. PollutionCtrl VRU compressor packages use Bitzer piston compressors or Copeland screw compressors, depending on the duty.
How a VRU compressor works
- Suction – Hydrocarbon vapor is drawn from tanks or loading operations into the compressor.
- Compression – A piston (Bitzer) or screw (Copeland) compressor raises the vapor pressure.
- Recovery – The compressed vapor is condensed or absorbed into liquid product for reuse.
- Return – Uncondensed gas returns to the vapor recovery loop, and recovered liquid is stored or returned to process.
Piston vs screw compressors for vapor recovery
| Type | Best suited for |
|---|---|
| Piston compressor (e.g., Bitzer) | Lower to medium vapor flow, high discharge pressure, flexible turndown |
| Screw compressor (e.g., Copeland) | Higher vapor flow, continuous duty, smooth operation |
Typical technical considerations
- Vapor flow and composition – determines compressor size and materials;
- Suction and discharge pressure – set by tank conditions and recovery pressure;
- Temperature control – interstage cooling for high-ratio compression;
- Safety – gas detection, pressure protection and explosion-proof design;
- Driver – electric motor with VFD for load variation.
Frequently asked questions
What is a vapor recovery unit compressor?
A VRU compressor boosts recovered hydrocarbon vapor pressure so it can be condensed or absorbed into liquid product, improving recovery efficiency.
What type of compressor is used in a VRU?
Piston compressors (such as Bitzer) suit lower to medium flow and high pressure; screw compressors (such as Copeland) suit higher flow and continuous duty. Selection depends on the vapor duty.
Why does a VRU need a compressor?
Most vapor recovery processes require the vapor pressure to be raised before condensation or absorption is practical; the compressor provides that pressure boost.
What is a Bitzer compressor used for?
Bitzer piston compressors are used in vapor recovery and refrigeration applications where medium flow, high pressure and flexible turndown are required.
What is a Copeland screw compressor used for?
Copeland screw compressors are used in higher-flow vapor recovery duty, providing smooth continuous compression with good efficiency.
How do I size a VRU compressor?
Sizing is based on vapor flow, composition, suction and discharge pressure, and operating schedule; the compressor package is engineered with the rest of the VRU.
How much does a vapor recovery compressor cost?
Cost depends on compressor type, vapor flow, discharge pressure and package scope. Send your vapor parameters for a preliminary budget estimate.
Do you supply VRU compressor packages?
Yes. PollutionCtrl supplies VRU compressor packages using Bitzer piston or Copeland screw compressors, integrated with the vapor recovery system and controls.
Request a project evaluation
Send your vapor flow, composition, tank pressure and recovery target for a VRU compressor recommendation.
How to select a VRU compressor
Compressor selection should follow the vapor source and recovery route. The key figures are suction pressure, discharge pressure, normal and peak flow, gas composition, temperature, liquid carryover risk and the required recovery destination.
- Confirm normal, minimum and peak vapor flow rather than one average value
- Check molecular weight, hydrocarbon range, moisture and corrosive components
- Control liquid carryover with suitable separation and drainage before compression
- Review hazardous-area motor, electrical and instrument requirements
- Allow access for oil, seal, valve, filter and control maintenance
A compressor package is only one part of the VRU. The separator, condenser, adsorption or absorption section, controls and safety devices must be checked as one process. Send the data from the VRU RFQ checklist for a preliminary review.
Compressor selection starts at the vapor source
A vapor recovery compressor cannot be selected from flow alone. The same flow can require a different machine when suction pressure, discharge pressure, molecular weight, condensing components, liquid carryover or duty cycle changes. The compressor, inlet separator, controls and recovery destination should therefore be reviewed as one package.
VRU compressor data sheet
| Item | Minimum information | Common problem when omitted |
|---|---|---|
| Flow | Minimum, normal and peak vapor flow | A unit that cannot turn down or cannot handle the loading peak |
| Pressure | Suction range and required discharge pressure | Tank pressure instability or insufficient downstream pressure |
| Composition | Hydrocarbons, moisture, air and corrosive components | Wrong materials, seal arrangement or condensation estimate |
| Liquid risk | Expected carryover and drainage conditions | Valve, seal or compressor damage |
| Operation | Continuous, batch or loading cycle | Excessive starts, overheating or poor control response |
| Site | Area classification, ambient range and utilities | Electrical or cooling package that does not match the site |
Reciprocating and screw packages
Reciprocating compressors are often considered where pressure ratio, gas volume and staged compression suit that arrangement. Screw compressors may be considered for steadier flows and a different operating envelope. Neither type is automatically better. The decision follows the gas data, turndown, liquid tolerance, maintenance resources and the required discharge condition.
Package scope to confirm
- Inlet knockout and level protection before the compressor
- Pressure, temperature and vibration monitoring appropriate to the machine
- Recycle or capacity control for changing vapor flow
- Relief, shutdown and ESD interfaces
- Drainage, ventilation, access and lifting space for service work
- Recommended startup spares and routine replacement parts
For a complete system review, see the oil and gas vapor recovery unit, installation and commissioning and spare parts service pages.
VRU Compressor Package Selection
The compressor is a critical part of a vapor recovery unit. Selection should consider suction pressure, discharge pressure, normal and peak vapor flow, gas composition, liquid carryover, temperature, turndown, duty cycle and hazardous-area requirements. A compressor package should be reviewed together with the separator, controls, valves and piping rather than as an isolated component.
VRU Compressor Service and Maintenance
Routine checks may include suction conditions, oil or seal condition, vibration, discharge temperature, liquid separation, control response and pressure protection. Provide the existing compressor model, operating data and failure symptoms when requesting replacement parts or troubleshooting support.
See the oil and gas VRU system, VRU spare parts service and VRU design guide pages for the complete project scope.