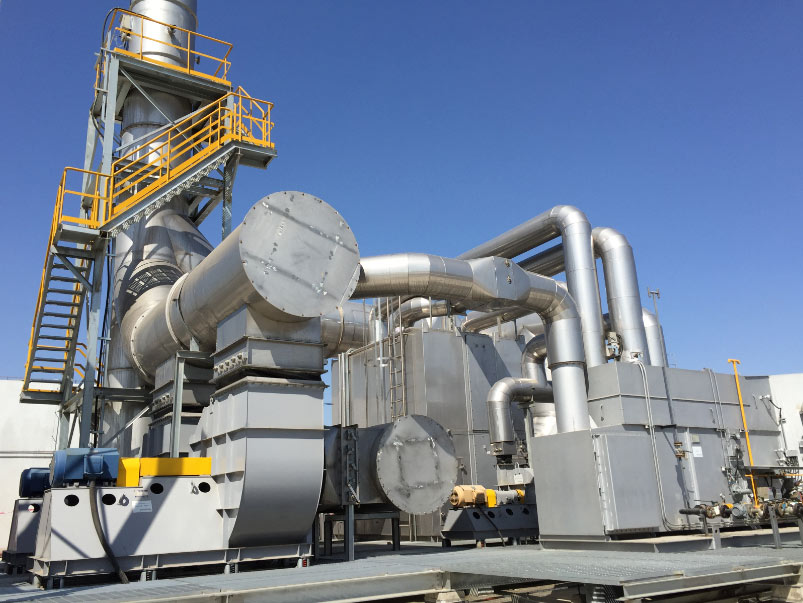
Sludge odor control captures and treats air displaced or released during storage and handling. Filling, mixing, emptying and opening a hatch can change the gas load quickly. A storage system therefore needs a defined collection arrangement and operating envelope, even when the strongest odor is intermittent.
This page focuses on sludge holding tanks and silos. For capture around presses, centrifuges and conveyors, use the sludge dewatering odor-control guide.
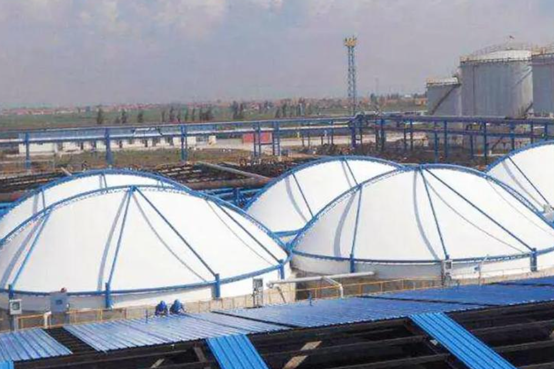
Review the storage cycle before selecting the fan
Record tank dimensions, headspace, normal liquid or solids level and the filling and emptying schedule. Include the longest storage period and any mixer operation. Note when doors or hatches are open, because those events change both the capture condition and the required airflow.
Air displaced during filling and odor generated while sludge is stored are different contributions to the duty. A steady average airflow may not describe the condition during truck loading, silo filling or an operational upset.
Storage design inputs
| Part of the system | Data to collect | Design decision |
|---|---|---|
| Cover or silo | Openings, seals and maintenance access | Containment and extraction arrangement |
| Filling and discharge | Rates, duration and simultaneous operations | Peak collection duty |
| Stored sludge | Type, residence time, temperature and handling | Sampling conditions and expected variability |
| Gas | H₂S, ammonia, relevant organics and humidity | Treatment route and materials |
| Duct and drains | Route, low points and condensate destination | Resistance, cleaning and corrosion protection |
Treatment selection for wet sludge air
Compare the complete gas-treatment process against measured normal and peak conditions. A wet stream may need droplet removal before a downstream reactor or media bed. Media life, fouling and drainage should be evaluated alongside power consumption.
Review low-temperature plasma equipment and microwave UV oxidation equipment as candidate oxidation routes. Require evidence for the specified gas and define any scrubber, demister or polishing stage needed around the reactor.
Practical maintenance checks
- Inspect hatch seals and extraction connections after maintenance.
- Track fan status, actual airflow and treatment pressure loss.
- Check condensate drains and avoid accumulation in low duct sections.
- Record the condition of media, lamps or discharge modules according to the installed process.
- Compare complaints with filling, mixing and unloading events.
A rising pressure drop and lower source airflow can indicate a collection problem even before an outlet measurement changes. Keep a commissioning baseline for comparison.
Use an acceptance test that includes the peak event
Agree the storage conditions under which the system will be tested. Record source capture, airflow and inlet/outlet gas data during the defined event. State the test method and outlet requirement in the purchase specification.
The EPA biosolids odor-control fact sheet provides general background on management and control methods. It is not certification of PollutionCtrl equipment.
Questions before ordering
Is a storage silo the same duty as a dewatering room?
No. A silo headspace and a room with several open machines have different capture arrangements. Specify each source separately before combining their air.
Can replacement media alone solve recurring odor?
Only if media performance is the cause. Check covers, airflow, condensate and changes in sludge operation as part of the investigation.