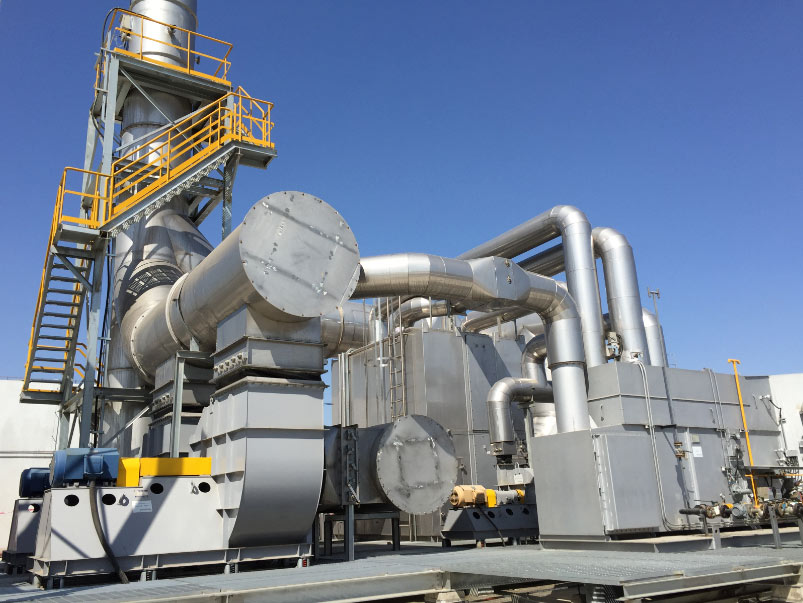
Coal-based granular activated carbon for air purification holds solvent vapours and odours on a microporous coal bed. This page covers when it fits, how gas adsorption differs from water treatment, the systems used and what decides bed life.
When Coal-Based GAC Fits a Gas-Phase Duty
Gas-phase adsorption works inside a defined window of conditions; outside it, carbon either blinds quickly or never holds the target.
| Condition | Suited to a coal GAC bed | What changes outside the window |
|---|---|---|
| Airflow | Low to moderate flows allowing a practical bed | Huge volumes mean huge vessels and high pressure drop |
| VOC concentration | Dilute streams, from trace odour to low solvent loadings | Adsorption heat creates hot spots and shortens bed life |
| Relative humidity | Dry to moderately humid air | Water competes for sites and cuts capacity; use impregnated carbon or dry the gas |
| Temperature | Ambient to warm exhaust; cool hot gas first | Capacity falls with temperature, and hot solvent-laden air risks fire |
| Dust and aerosols | Clean gas after filtration and demisting | Dust and oil mist plug the bed and raise pressure drop |
Outside it, the answer is not a bigger vessel but a different route: carbon is often one stage of a wider VOC treatment system.
Why Gas-Phase Adsorption Needs a Specific Pore Size and Particle Size
In water treatment the adsorbate is dissolved, so surface area and iodine number dominate selection: powdered activated carbon is simply dosed into the stream, and liquid-phase grades such as GAC for sewage treatment are chosen on capacity and hydraulics.
In gas service the molecule must cross the gas film, travel the macropore and mesopore network and reach a micropore. Any step can limit performance, so pore size distribution must match the molecule: micropores do the work on low-molecular-weight solvents and odours, while macropores and mesopores are the transport channels.
Particle size is the same trade-off: finer granules reach working capacity faster but cost more pressure drop, while coarse 4×6 and 4×8 mesh grades suit high-flow duties. Pelletized forms are low-dust and crushed granular forms cheaper, and a structured honeycomb activated carbon suits beds where pressure drop binds. Impregnated grades extend the range to hydrogen sulfide, sulfur dioxide and mercury, and a coconut shell carbon is common where hardness is the priority.
Typical Technical Data
| Parameter | Typical range |
|---|---|
| Appearance | Granular, crushed or pelletized |
| Iodine number | 800-1100 mg/g |
| CTC activity | 50-75% |
| Hardness | 95% min |
| Moisture content | 5% max |
| Ash content | 10% max |
| Particle sizes | 4×6, 4×8, 8×30 mesh and others |
Specifications vary with grade. Coal-based GAC comes from selected bituminous coal or anthracite feedstocks; activation develops the microporous structure behind its gas-phase capacity.
System Configurations Used in Practice
Single fixed-bed adsorbers
The base case is one vessel with a supported bed, inlet distributor and fines filters. Bed depth, cross-section, superficial velocity and empty bed contact time are the design parameters.
Parallel, staged and multi-layer beds
For larger flows, vessels run in parallel so total cross-section keeps velocity acceptable. In lead-lag operation the lead bed does the bulk of the work and the lag bed polishes the outlet, so the lead can be changed out while the lag protects the stack. Multi-layer vessels run a distribution layer, the working grade and an impregnated layer where acid gases are present.
Pairing with rotary concentrators and oxidizers
Where exhaust is very dilute but large, carbon alone would mean an impractical vessel. A rotary concentrator adsorbs organics onto rotating media and releases them into a much smaller desorption stream, which then goes to a carbon bed, a regenerative thermal oxidizer or another oxidizer. Carbon also serves as a downstream polishing stage.
Design Points That Decide Bed Life
Residence time and bed velocity
Two numbers carry the design: empty bed contact time (bed volume divided by actual flow) and superficial velocity. Contact time must let the target compounds reach working capacity; velocity must keep pressure drop and attrition within budget.
Pressure drop monitoring and changeout criteria
Differential pressure is the cheapest continuous indicator of bed condition: a rising trend points to dust loading, compaction or fines migration, a sudden drop to a channel or bypass. Baseline at commissioning, alarm on a defined increase, and confirm by outlet monitoring. Changeout follows breakthrough, not pressure drop alone.
Dust and moisture pre-treatment
Pre-treatment protects the capacity you paid for: a pre-filter for particulate, a demister for oil mist, condensate removal with a maintained drain, and reheat or insulation so the gas arrives above its dew point.
Fire safety and temperature monitoring
Adsorption releases heat, and ketones, aldehydes and unsaturated hydrocarbons can oxidize on carbon and drive it further. Measures: temperature probes in the bed with high-temperature alarm and shutdown, avoiding high solvent loadings on one bed, cooling hot exhaust before the carbon, and earthing of vessel and ducting during changeout.
Combining Carbon Adsorption with Catalytic Combustion
Adsorption and catalytic combustion are complementary. Carbon holds organics; a catalyst destroys them at lower temperature than thermal oxidation, if the stream is free of poisons. Carbon can act as a concentrator feeding a much smaller catalytic oxidizer, or as a guard bed protecting catalyst downstream. Halogen, silicone or heavy-metal content must be identified before catalyst is specified, and the route is normally settled in a wider adsorption and catalytic combustion evaluation.
Replacement, Regeneration and Spent Carbon
Regeneration only makes sense where solvent value or replacement cost justifies the equipment and losses. Steam regeneration suits solvent recovery and returns the bed to service on site, but consumes steam, produces condensate that must be treated, and does not restore capacity indefinitely. Thermal reactivation off site covers other cases, with some capacity and media lost each cycle.
Impregnated carbon is generally not regenerated, because the impregnant is consumed and cannot be restored in place. Carbon carrying halogens, mercury or mixed contaminants goes to reactivation or disposal rather than reuse. Characterize spent carbon before disposal, since it may fall under hazardous waste rules.
Information We Need to Specify a Carbon Bed
Send airflow at operating conditions, the compounds and their concentration ranges, inlet humidity and temperature, particulate and oil mist loading, and the pressure drop budget.
Engineering support covers grade selection, contact time, pressure drop and replacement planning. Media ships in 25 kg bags, 500 kg bulk bags or customized packaging, stored dry, sealed and away from oxidising agents.
Frequently Asked Questions
How do I know when gas-phase carbon is saturated?
Monitor the outlet, not the media. Concentration trending toward the limit, or a defined rise in differential pressure, triggers sampling; laboratory analysis of a media sample shows how much working capacity remains.
Can coal-based granular activated carbon be regenerated?
It depends on what it has adsorbed. Steam regeneration works for single-solvent recovery and thermal reactivation off site suits other cases. Impregnated grades, and carbon carrying halogens, mercury or mixed contaminants, are normally not regenerated.
Which particle size should I choose for a gas-phase bed?
Start from the binding constraint: where fan energy and pressure drop dominate, a coarser 4×6 or 4×8 mesh grade is usually right; where a low outlet concentration matters at moderate flow, a finer 8×30 grade gives faster kinetics.
Does humidity reduce VOC removal?
Yes. Water competes for the same adsorption sites, so working capacity for organics falls as humidity rises. On humid gas, pre-treatment to cut moisture, or an impregnated grade, is part of the design.
Can coal carbon be used after a rotary concentrator?
Yes, and it is a common arrangement. Concentrating first reduces the gas volume to be treated, which either shrinks the carbon vessel needed or makes carbon viable where the raw volume would have ruled it out.
Talk to an Engineer
Send your stream conditions – flow, compounds, concentration, humidity, temperature and particulate loading – and we will return a recommended grade, an indicative bed design and a changeout strategy. Contact our engineers to start.